logotipo

Custom Bottle Molding:
In-House Design, Tooling & Manufacturing

Turn an original packaging concept into a repeatable production system with Jarsking’s integrated custom bottle molding and tooling services. From structural design and prototyping to steel mold fabrication, trial production, validation, decoration, and bulk delivery, our teams coordinate the complete glass or plastic packaging program—reducing handoff delays while strengthening quality, consistency, and control.

Before commissioning new tooling, we assess whether your project can use one of our 30,000+ existing molds, adapt a proven packaging platform, or requires a fully custom private mold.

Why In-House Molding Is a Competitive Advantage

Most packaging suppliers outsource mold development to external toolmakers, creating handoff delays, version control gaps, and IP exposure. When your mold is built and held in-house, your brand’s unique bottle silhouette stays protected — and every production run pulls from the same validated tooling.

Design-to-tooling under one roof

Structural engineers and mold designers collaborate directly, eliminating translation errors between concept and production spec.

Pilot runs before mass production

Small trial batches catch issues before you’re committed to 50,000 units.

30,000+ existing mold library

Repurpose proven preform structures to cut tooling costs and compress timelines.

IP security

Molds are held exclusively in Jarsking’s facility; no third-party access.

Faster sampling cycles

Priority scheduling on in-house tooling vs. queuing at external toolmakers.

Custom Bottle Molding Capabilities

Explore Jarsking’s custom bottle molding capabilities across glass and plastic packaging. From material selection and molding processes to closures, structural development, decoration, and quality planning, we coordinate each requirement as one production program. The overview below helps buyers compare available options, development routes, and project-specific commercial requirements before requesting quotations.

ParameterAvailable options
Packaging typesBottles, jars, vials, caps, overcaps, collars, pumps, sprayers, droppers, and related components
Primary materialsGlass, PET, PE, and PP; other materials are evaluated per project
Production processesGlass container forming, plastic injection molding, stretch blow molding, extrusion blow molding, and component assembly
Development routesExisting mold, modified platform, OEM, ODM, and fully custom OBM
ClosuresScrew, snap-on, crimp, pump, sprayer, dropper, disc cap, and project-specific dispensing systems
Structural customizationBottle silhouette, capacity, neck finish, wall structure, base, closure interface, embossing, and debossing
Color and decorationPantone color matching, coating, frosting, screen printing, hot stamping, metallization, labeling, and related finishes
Quality planningDimensional inspection, functional testing, compatibility testing, AQL sampling, and lot traceability as applicable
Existing-mold MOQ10,000 pieces per SKU
Custom-mold MOQ30,000–50,000 pieces per SKU, confirmed per project

What Does a Private Mold Actually Mean?

A private mold is production tooling developed for a bottle or component that is not selected directly from an existing shared mold library. It may create a proprietary bottle silhouette, structural feature, closure interface, embossing pattern, or complete packaging system.

Private-label packaging

normally uses an existing bottle or jar customized with the brand’s color, logo, decoration, and secondary packaging

Private-mold packaging

requires new structural tooling to produce an original physical form

Semi-custom packaging

retains proven elements—such as a neck finish, preform, closure platform, or base structure—while modifying parts of the design

Ownership, exclusivity, permitted use, storage, maintenance, modification, and transfer terms should be stated clearly in the tooling quotation and agreement.

Tooling vs Molding

Many buyers compare the tooling charge with the price of one finished bottle. However, these costs cover different activities.

TermWhat it coversWhen the cost occurs
Product designAppearance, proportions, user experience, and brand expressionDevelopment stage
Structural engineeringCapacity, wall structure, neck fit, closure interface, mold release, and manufacturabilityBefore tooling
ToolingEngineering and manufacturing the production mold systemMainly an upfront investment
MoldingOperating the approved tool to manufacture bottles or componentsEvery production order
DecorationCoating, printing, frosting, metallization, hot stamping, or labelingEvery production order
Testing and QCDimensional, visual, functional, compatibility, and shipment checksDevelopment and production

A production mold is therefore not simply a metal copy of the bottle. It is a working manufacturing system designed to form the product consistently over repeated production cycles.

How Custom Bottles Are Molded

The correct forming process depends on the packaging material, bottle geometry, closure system, formula, decoration, production volume, and performance requirements. Glass bottles and plastic bottles should not be treated as if they use the same process or tooling.

Vidrio
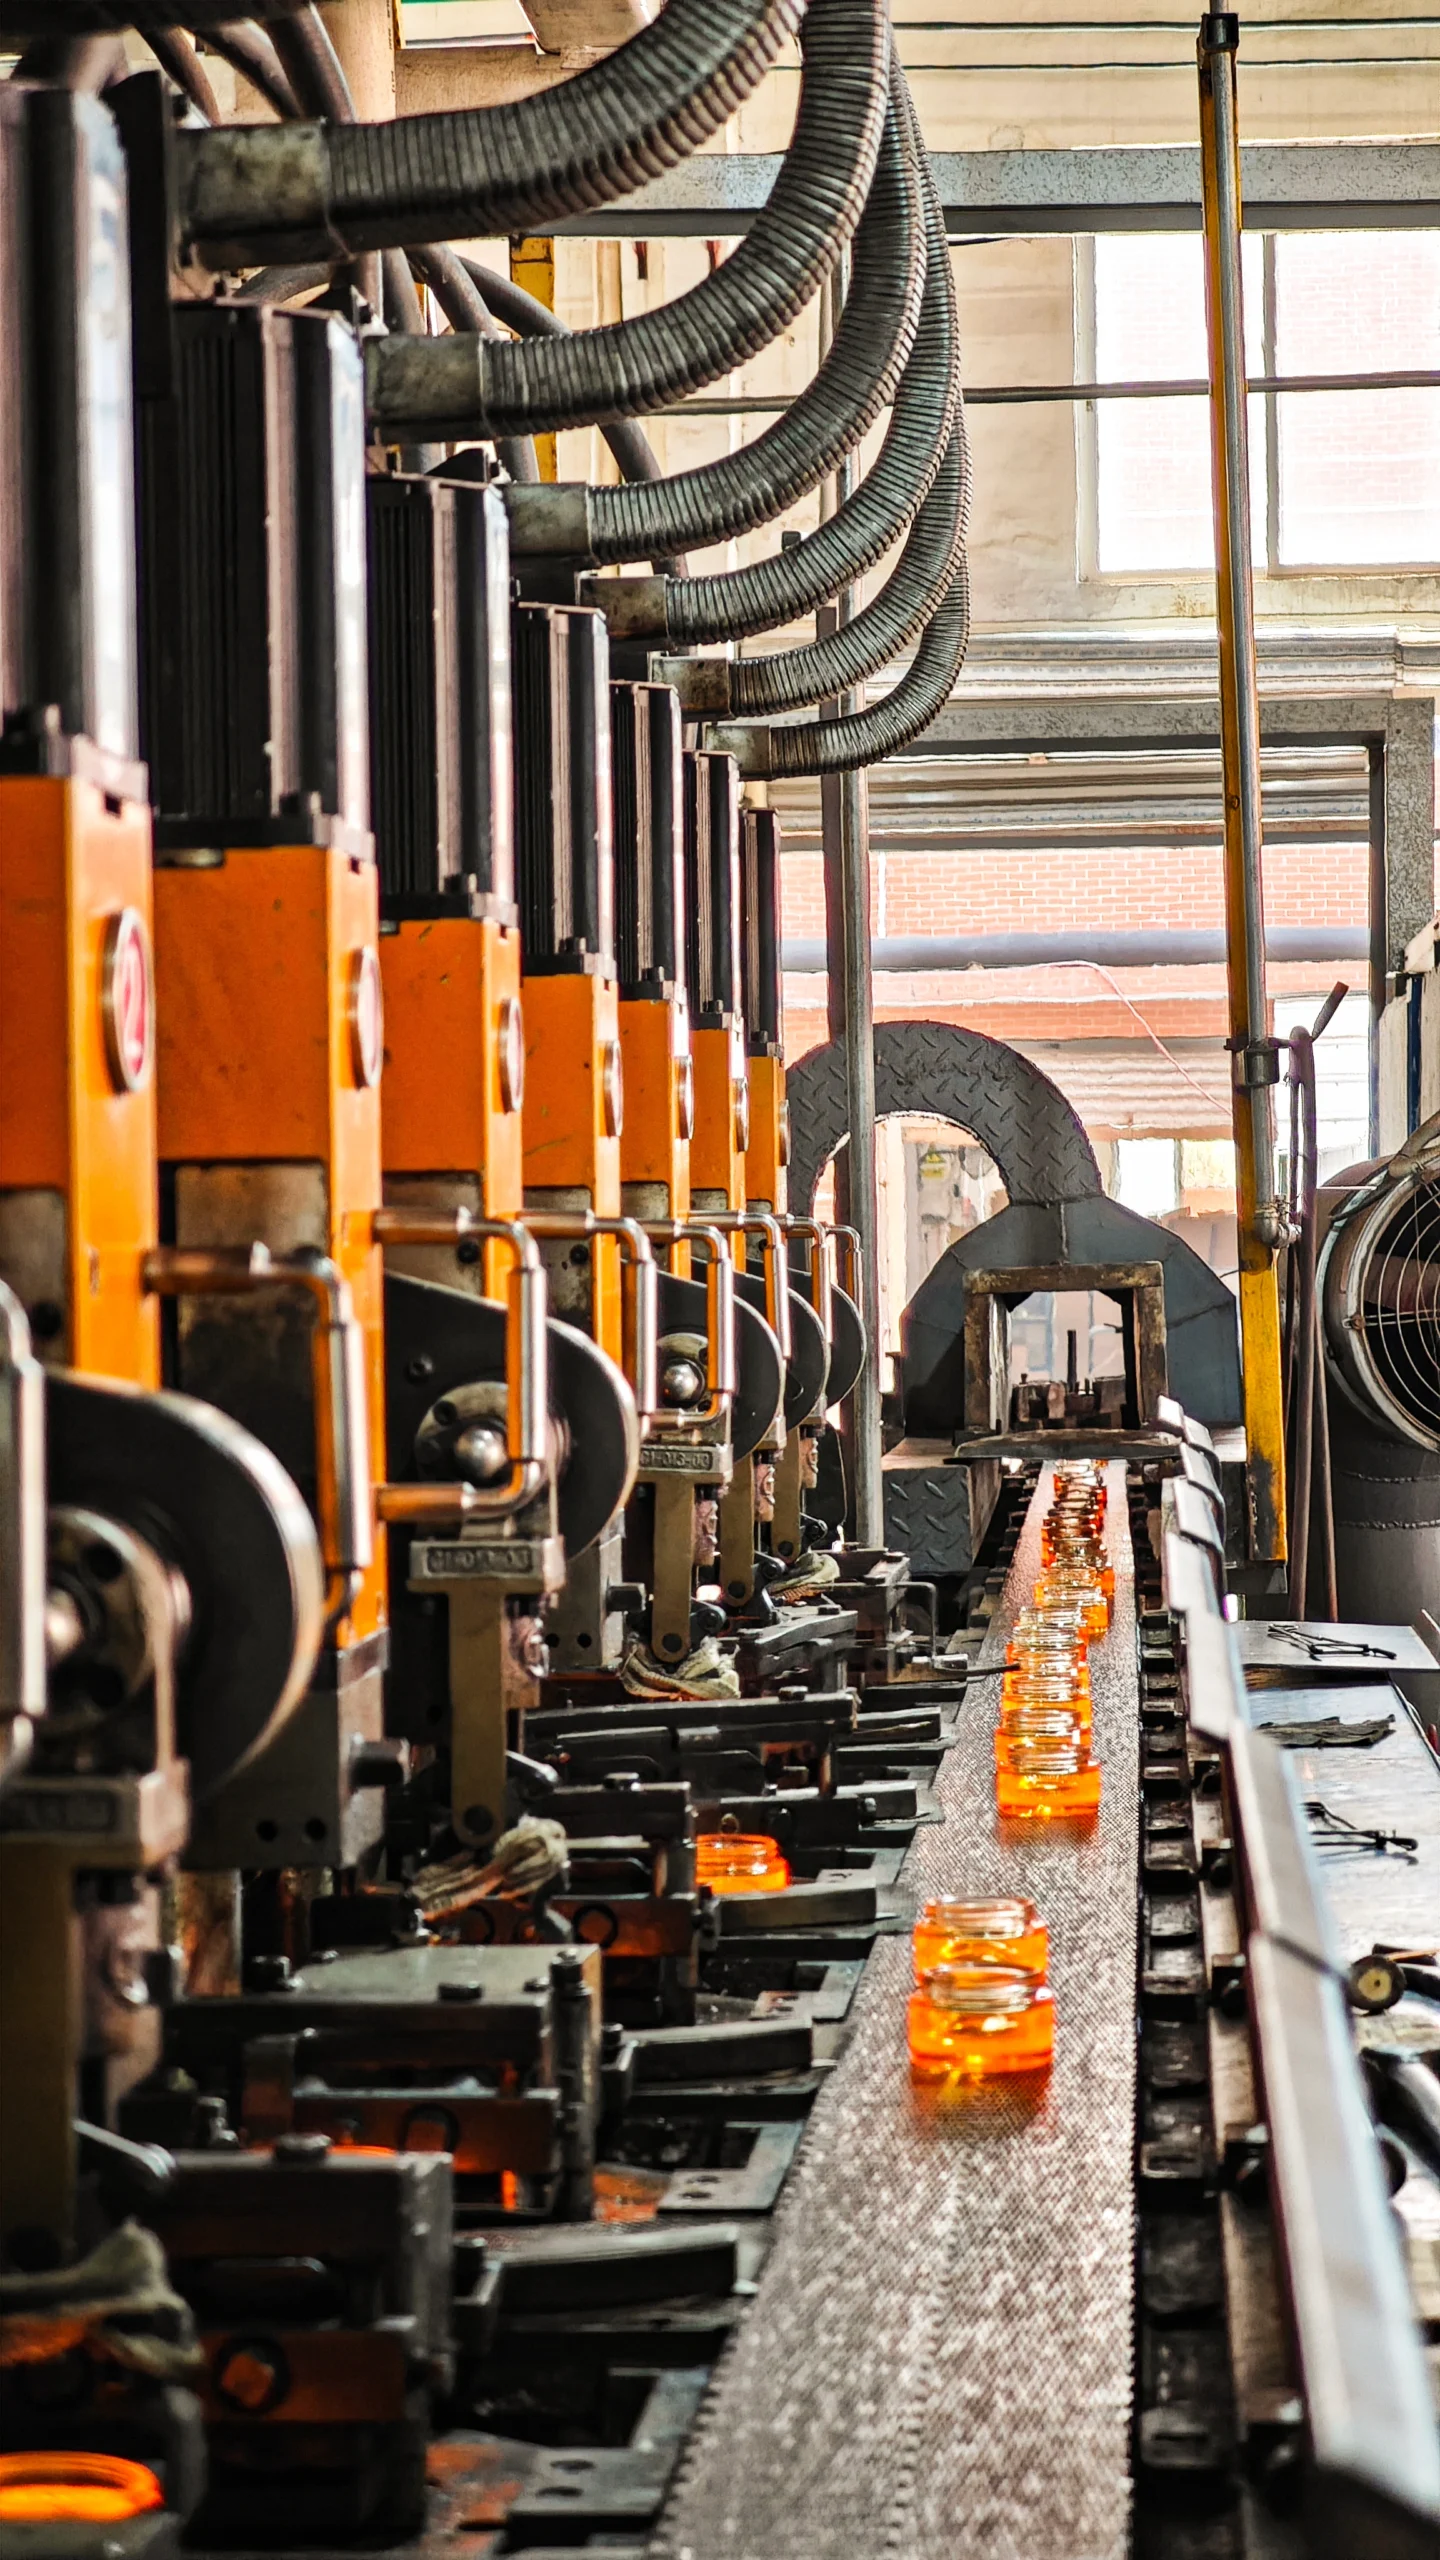
Manufacturing line with industrial machinery — Jarsking cosmetic packaging factory

How Glass Bottles Are Formed

Raw-material melting → glass gob forming → blank mold → parison → transfer → blow mold → annealing → inspection

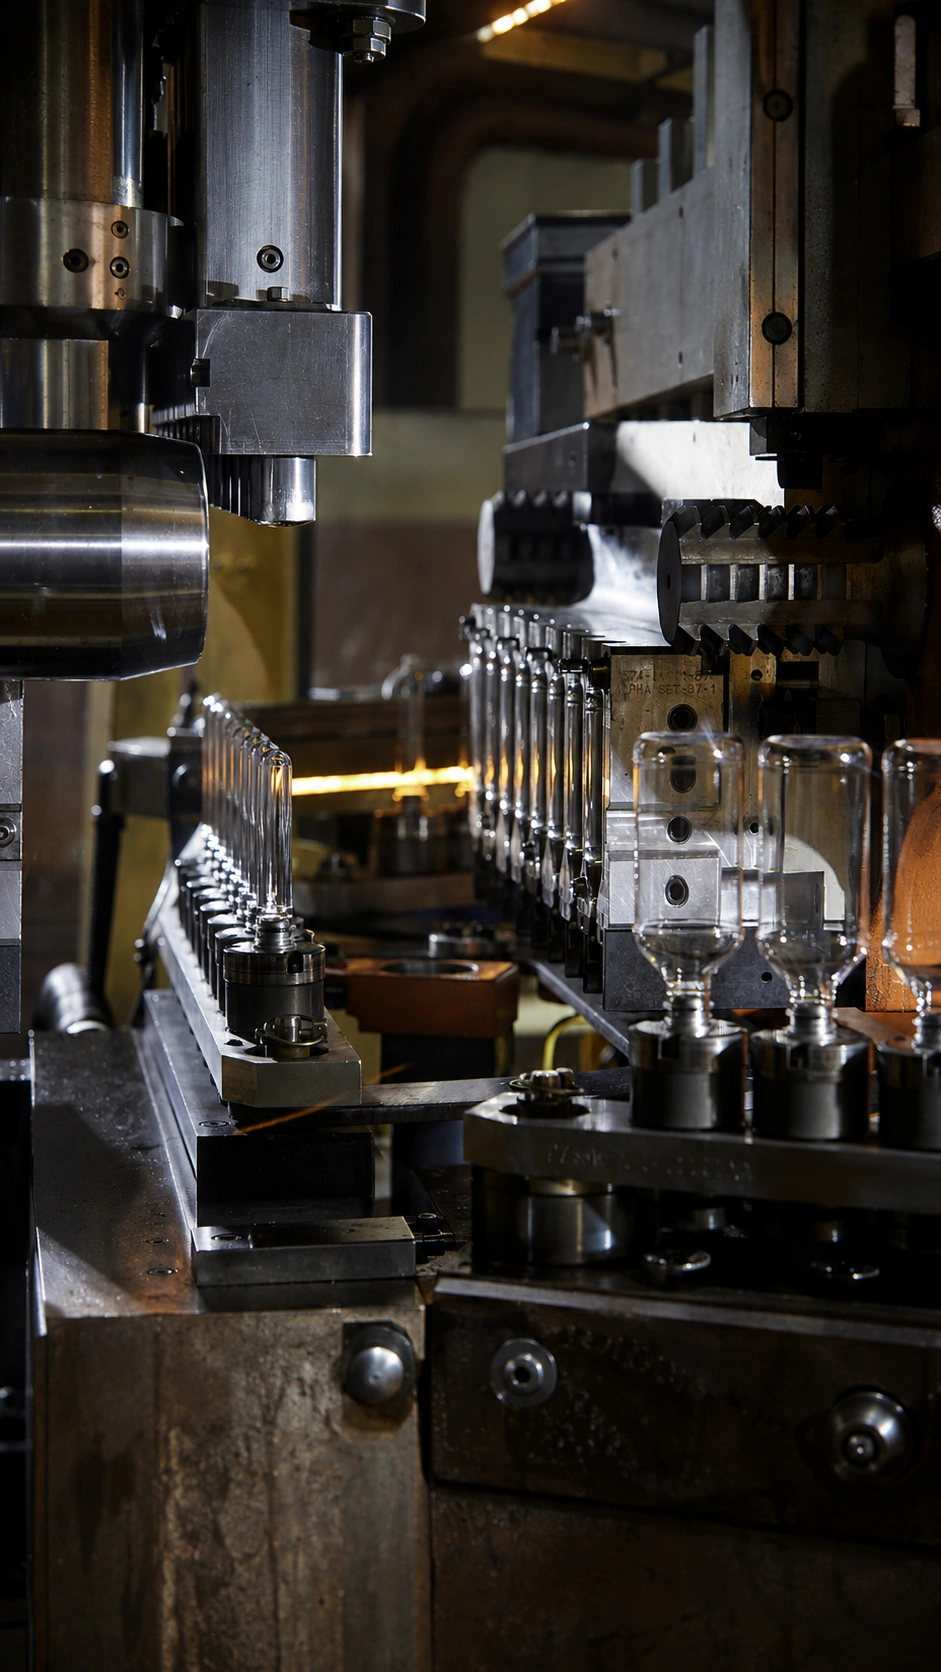
During glass container production, a measured portion of molten glass—called a gob—enters the first forming station. The blank mold creates an intermediate container form called a parison. That parison is transferred to the final blow mold, where air pressure forms it against the mold surface.


Blow-and-blow and press-and-blow are two established glass-forming methods. The selected method depends on the container format, neck, geometry, weight, production line, and required glass distribution.


A glass bottle tooling package may include several matched pieces of mold equipment:

  • Blank molds
  • Blow molds
  • Neck rings
  • Bottom plates
  • Baffles
  • Plungers, where required
  • Related inserts and forming components


These pieces must work together accurately. Their junctions influence seams, neck formation, base geometry, surface appearance, and dimensional consistency. This is one reason custom glass tooling is more complex than making a single bottle-shaped cavity.

MASCOTA
plastic mold forming
plastic bottle blowing

How PET Bottles Are Molded

PET resin → injection-molded preform → reheating → stretching → high-pressure blowing → cooling → inspection

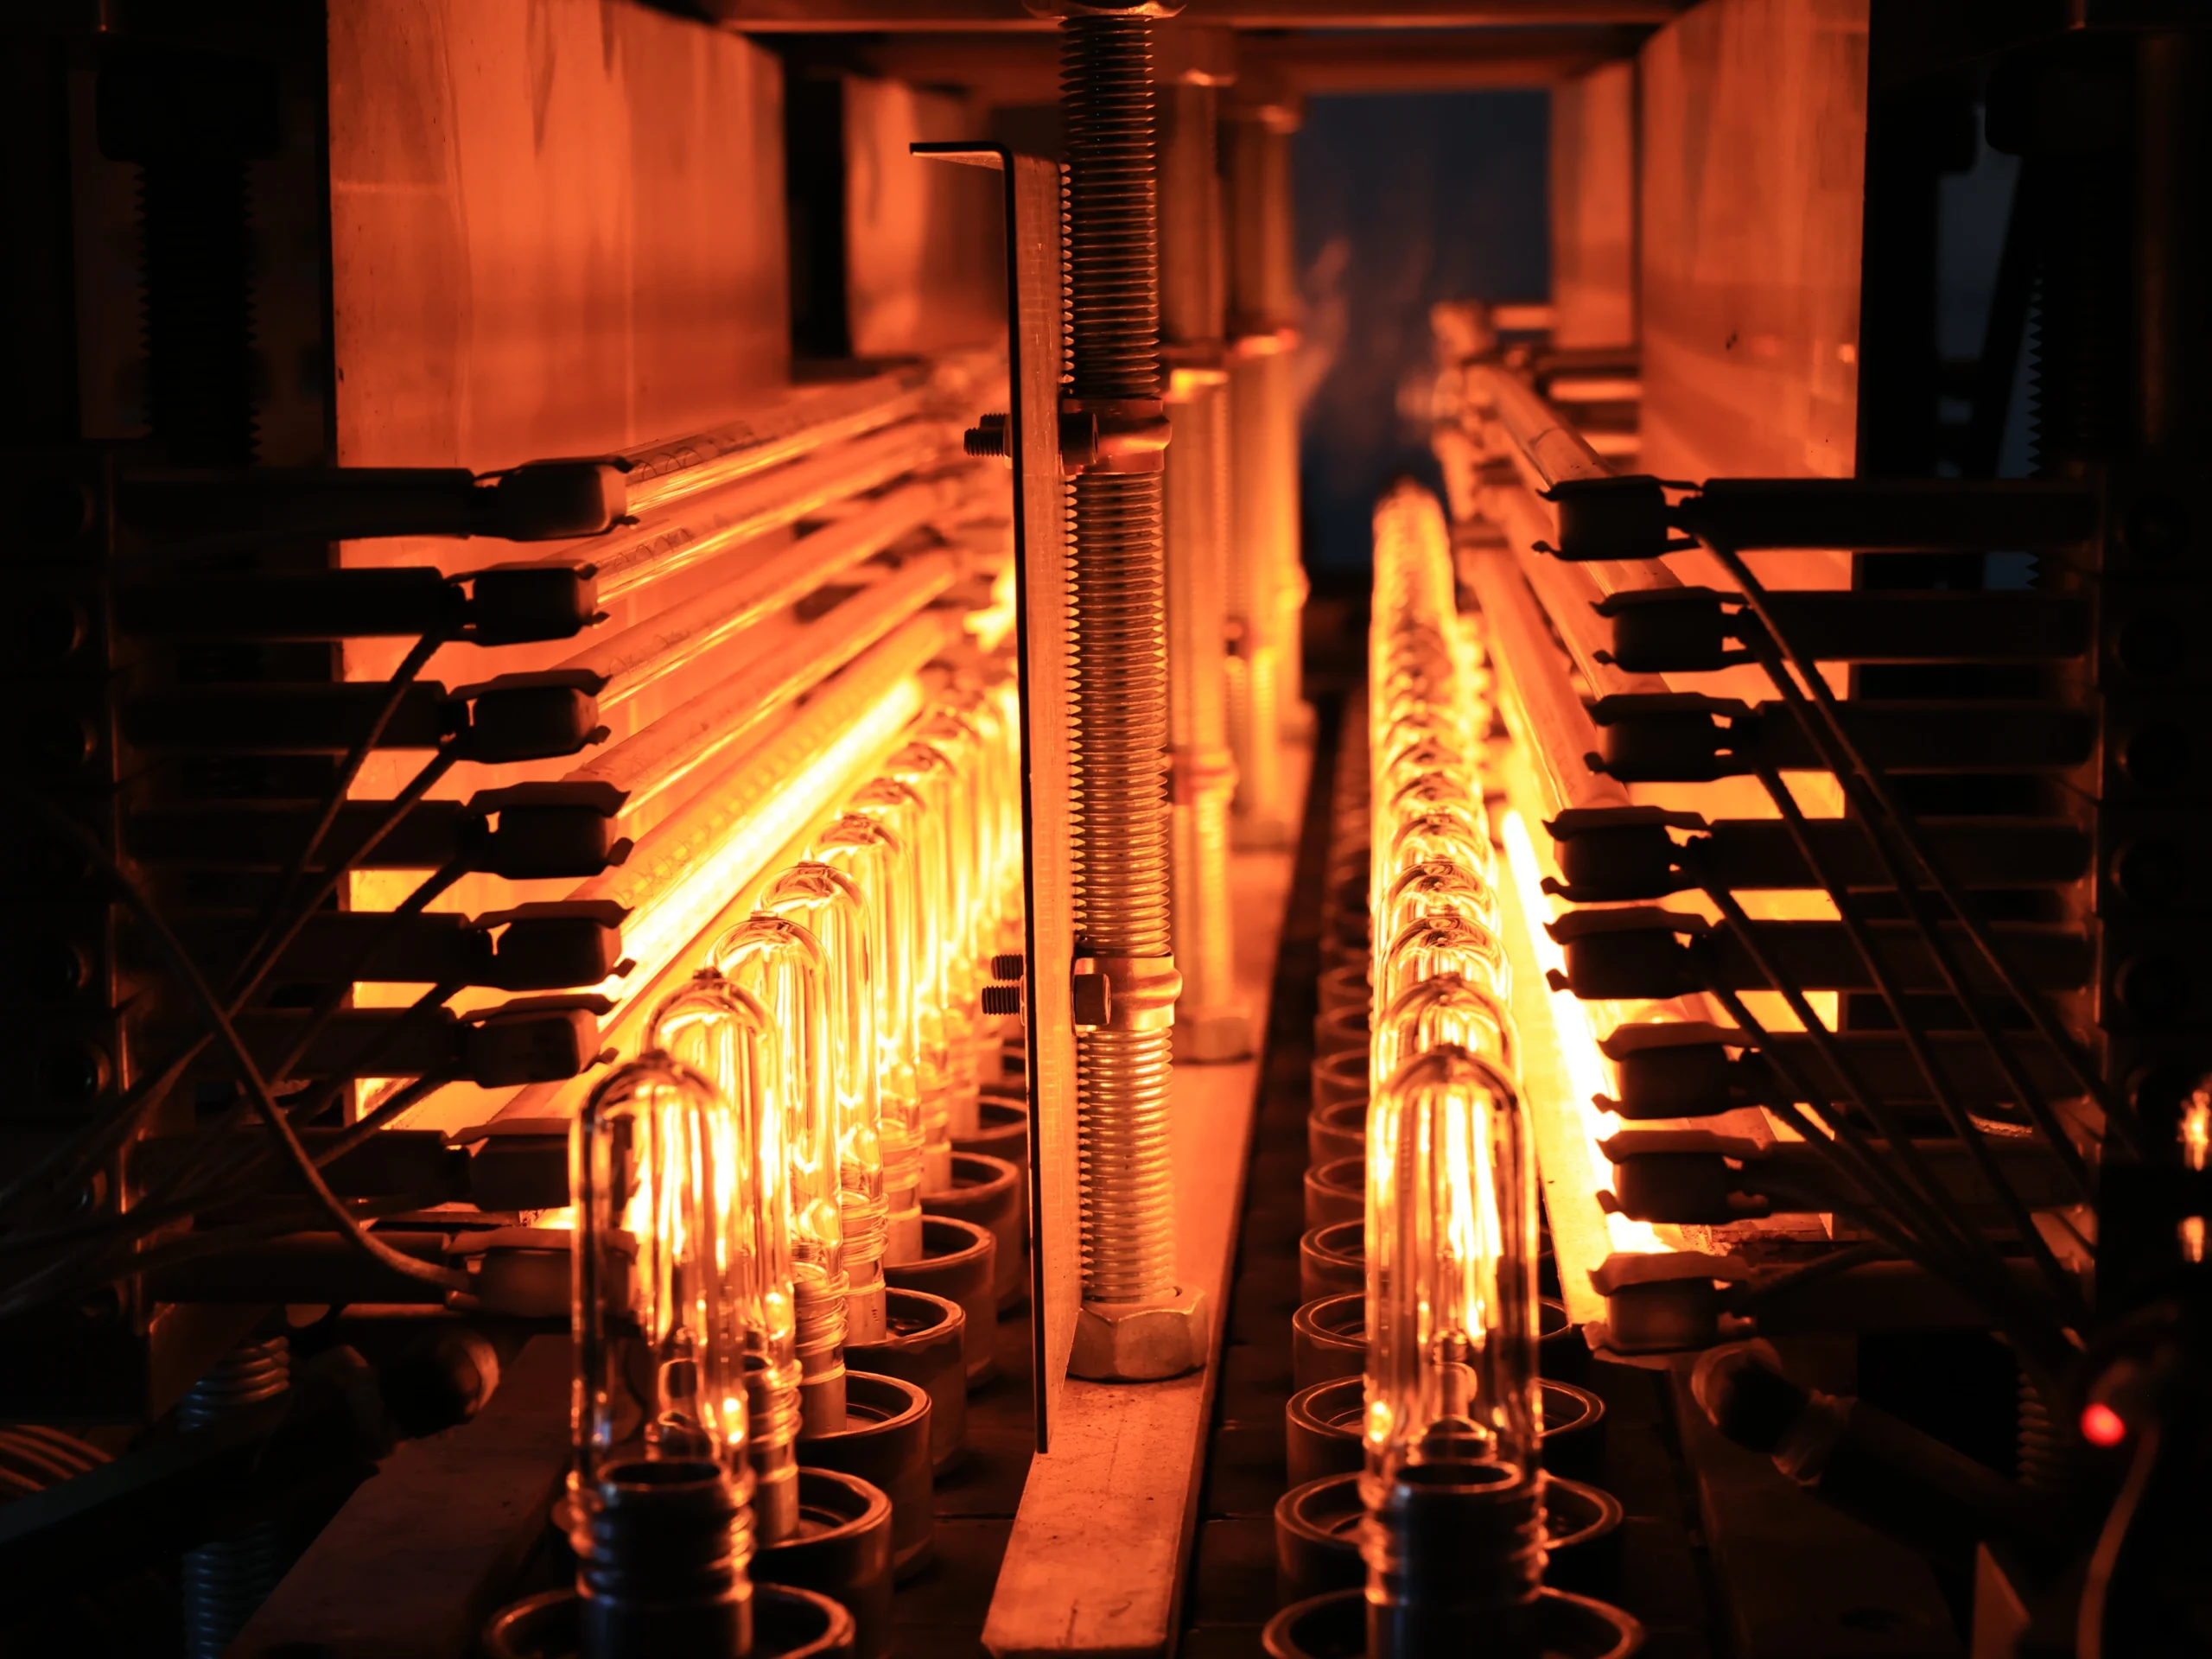
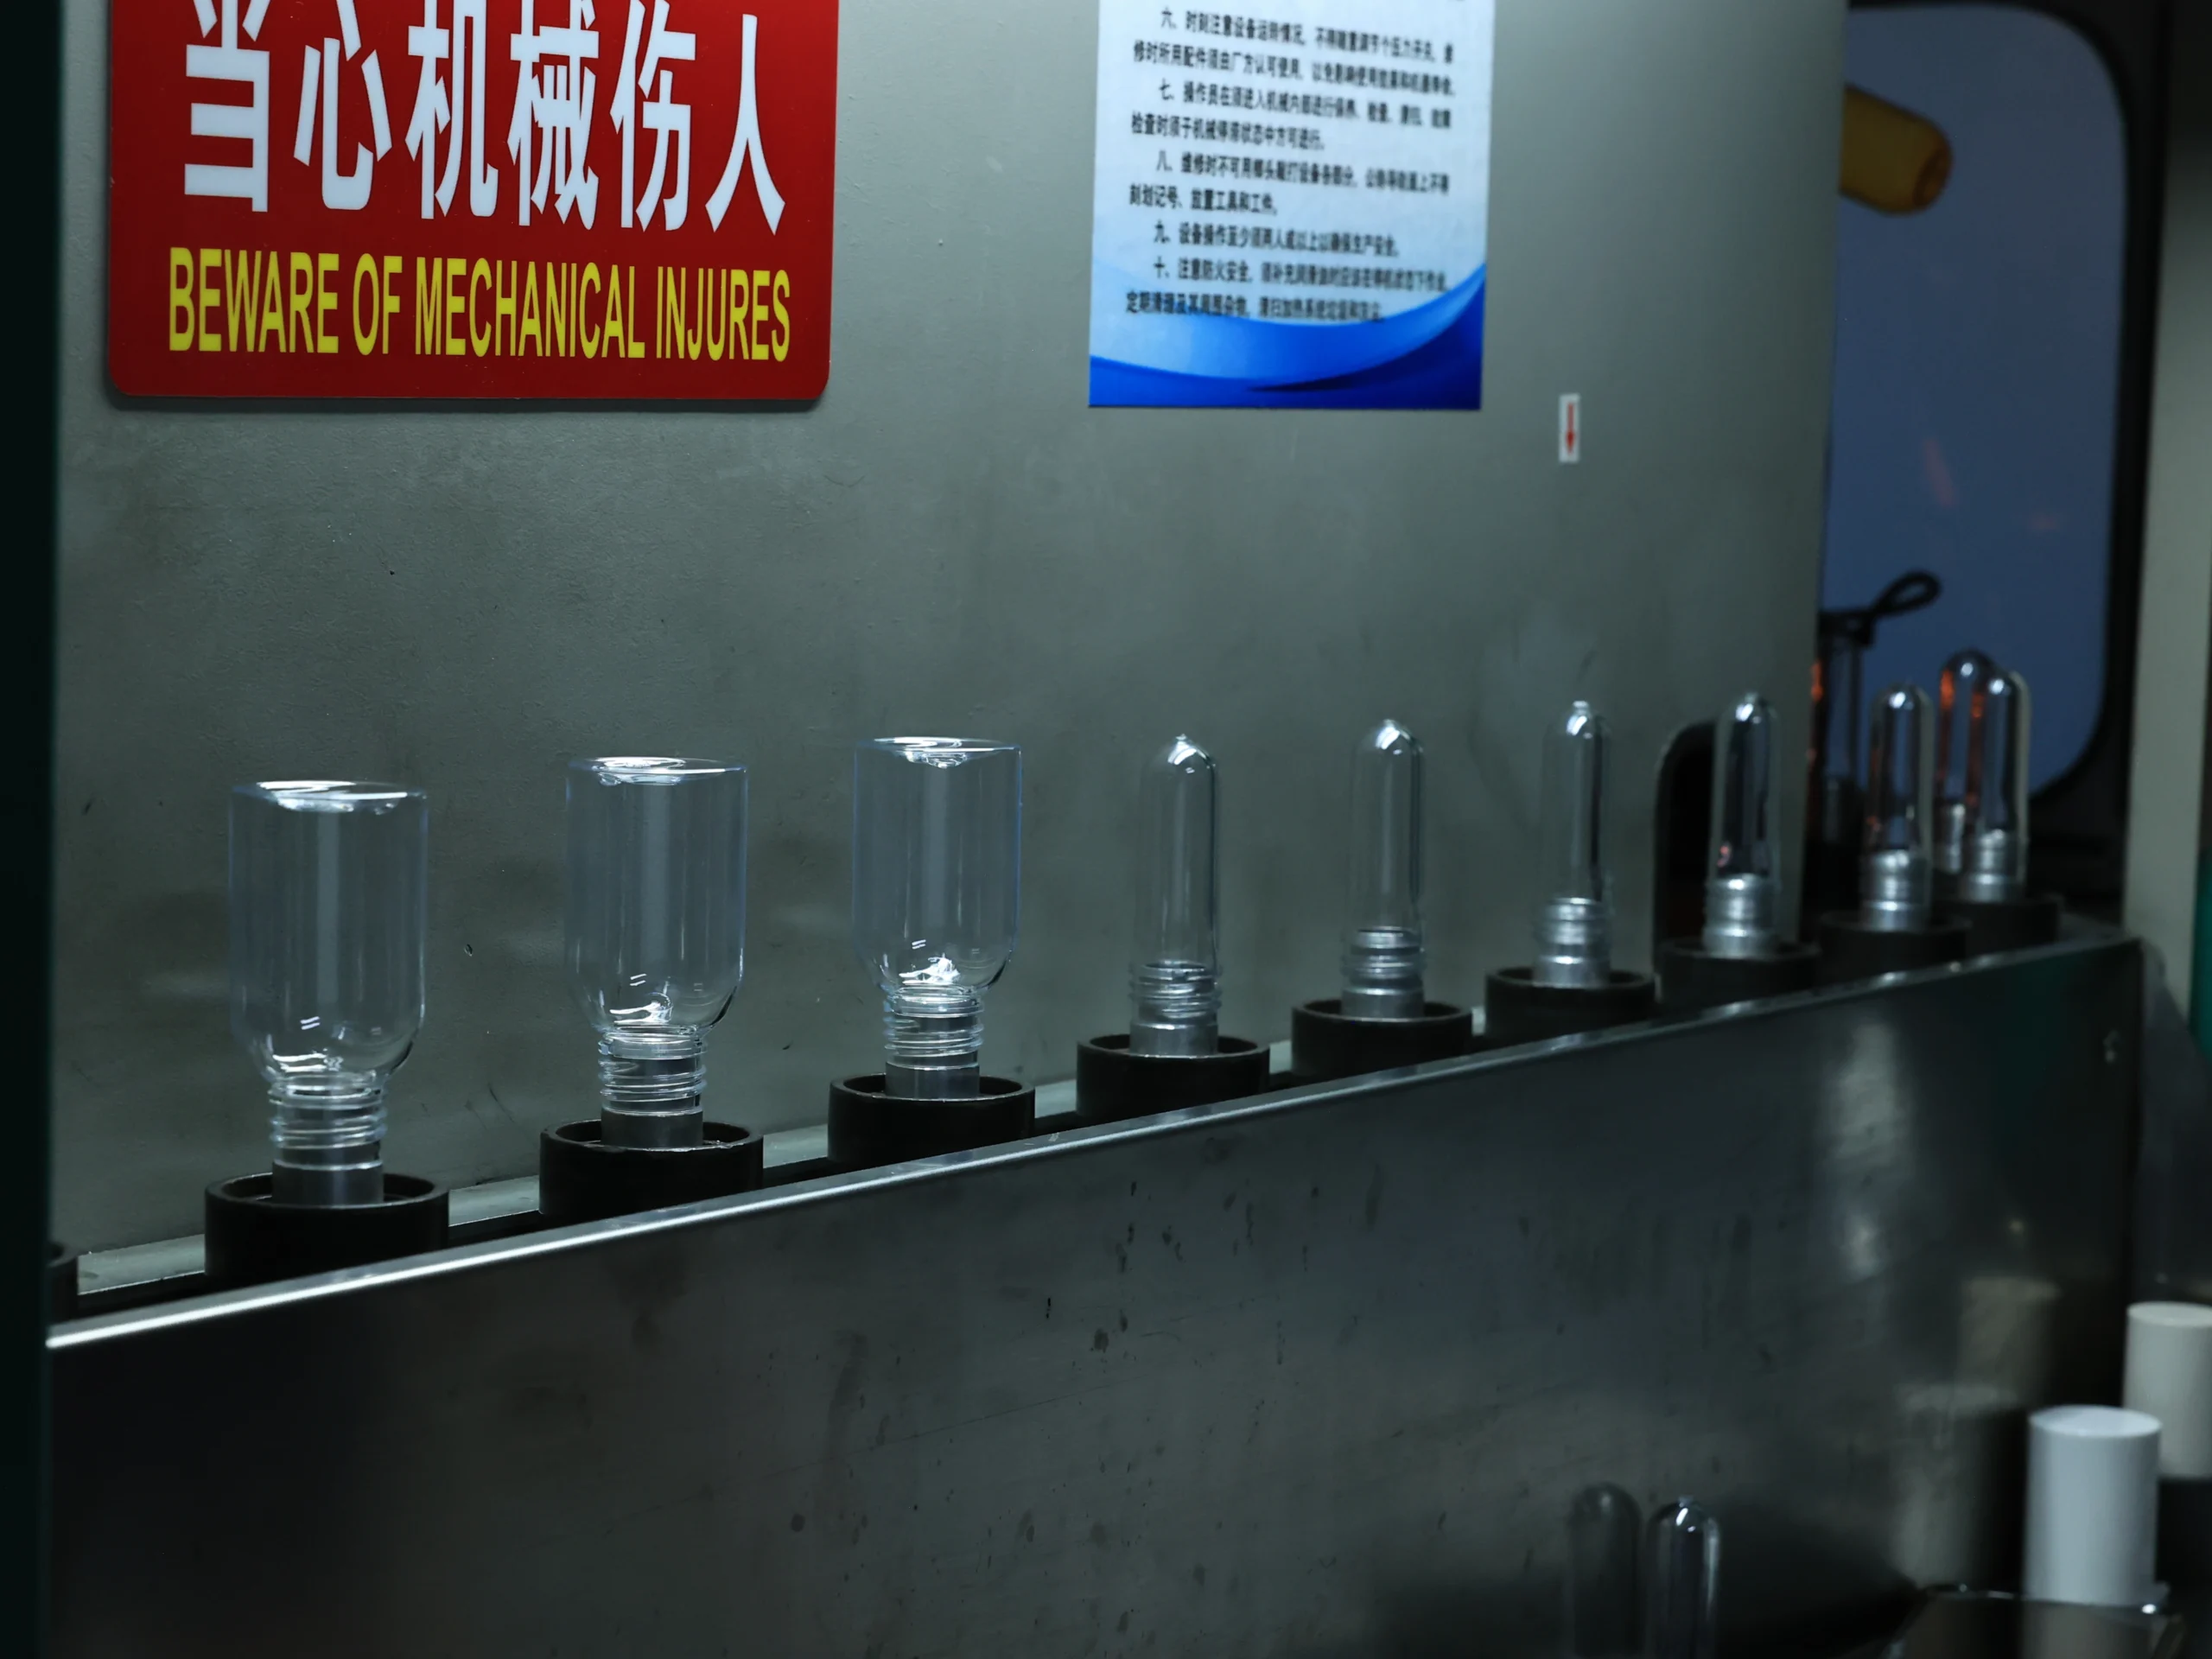
A PET bottle normally begins as a preform: a compact, tube-shaped part made by injection molding. Its neck finish is formed at this stage.


The preform is reheated and placed inside the bottle mold. A stretch rod extends it vertically while high-pressure air expands the material outward against the mold wall. This simultaneous axial and radial stretching helps develop the final bottle’s strength and material distribution.


Depending on the project, custom development may require:

  • Only a new bottle blow mold
  • A compatible existing preform with a new bottle mold
  • A custom preform and bottle mold
  • Separate tooling for the cap, overcap, collar, or dispensing component


Preform weight, neck dimensions, bottle proportions, material distribution, and blow conditions must be evaluated together. A visually attractive bottle mold cannot compensate for an unsuitable preform design.

PE & PP
PP bottle molding

How PE and PP Bottles Are Blow Molded

Resin melting → hollow parison extrusion → mold closing → pinch-off → air blowing → cooling → opening → trimming → inspection

In extrusion blow molding, heated plastic is extruded as a hollow tube called a parison. The two mold halves close around it, seal the lower area, and define the outer bottle shape. Air then expands the material against the mold walls.


The tool must control:

  • Bottle geometry
  • Neck and closure fit
  • Base and pinch-off formation
  • Material distribution
  • Cooling
  • Shrinkage
  • Parting lines
  • Bottle release
  • Trimming requirements


This process is frequently considered for squeezable and functional packaging made from materials such as PE or PP. Final suitability depends on the formula, bottle design, dispensing system, decoration, and filling requirements.

Components
jar components
bottle cap packing

How Injection-Molded Packaging Components Are Made

Clamping → material injection → packing → cooling → mold opening → ejection

Injection molding is used for many rigid packaging components, including caps, overcaps, collars, jar parts, actuator components, and dispensing-system pieces.

Molten resin is injected into a closed metal mold. After the component cools and stabilizes, the mold opens and the part is ejected.


A complete packaging system may therefore require several tools:

  • Bottle or jar tool
  • Inner component tool
  • Cap or overcap tool
  • Collar tool
  • Actuator or pump-component tool
  • Assembly fixtures or gauges


A custom package should be budgeted as a system, not only as its most visible bottle.

The 5-Stage Custom Mold Development Process

From first brief to production-ready bottle — here’s exactly how each stage works, what you’ll need to prepare, and what to expect at every step.

Stage 1: Brief & Feasibility Review

Timeline: Day 1–2

This is the conversation that sets the entire project up for success. You’ll share your brand vision, and our product development engineers will immediately assess whether your concept is manufacturable — and at what cost.

What you need to bring

  • Target fill volume (e.g., 30ml, 50ml, 100ml)

  • Material preference — glass, PET, PE, or PP

  • Decoration intent — frosted, coated, hot-stamped, screen-printed

  • Retail channel — luxury countertop, e-commerce shipper, pharmacy shelf

  • Reference images, mood boards, or a competitor sample you admire

moodboard sample

What Jarsking delivers

  • A written Feasibility Summary outlining recommended material, estimated tooling cost range, and structural constraints

  • A clear recommendation: Can your concept use an existing mold from our 30,000+ library, or does it require new steel tooling?

What to watch out for

  • Vague briefs produce vague quotes. The more specific your brief, the more accurate our feasibility timeline and cost estimate will be.

  • If you have a hard launch deadline, state it here — it determines which mold path (OEM ODM OBM) is right for you.

  • Screen captures of colors are not accepted for color specs. Have Pantone codes or a physical reference sample ready before Stage 3.

Stage 2: 3D Concept Rendering & Structural Engineering

Timeline: 1–8 days
(depending on complexity)

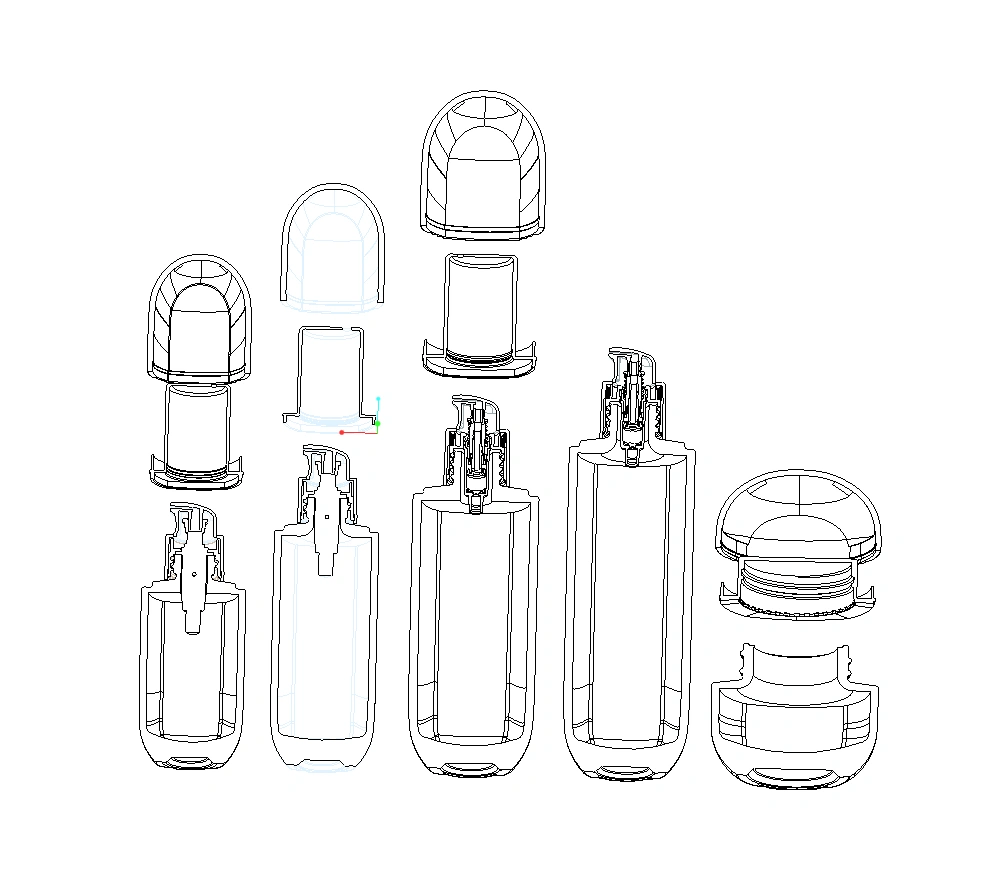
This is where your bottle takes visible shape. Our designers produce photorealistic 3D renders while structural engineers simultaneously validate the architecture behind the beauty.

What Jarsking delivers

  • Photorealistic 3D renders from multiple angles, with realistic lighting and surface finish simulation

  • Engineering specification sheet covering: wall thickness, draft angles, parting line placement, and neck finish specs

  • Material compatibility note — confirming the chosen resin or glass composition is compatible with your target formula

sketch and 3D demo

What you need to do

  • Review renders and give consolidated feedback. Avoid giving feedback in multiple rounds from different stakeholders — consolidate your team’s input into one marked-up document per revision round to prevent scope drift and delays.

  • Confirm label area dimensions, cap fitment type (screw, snap, crimp), and any surface texture requirements.

What to watch out for

  • Design details that look great in 3D can create manufacturing challenges. If our engineers flag a concern (e.g., undercuts, extremely thin walls, sharp internal corners), take it seriously — these will affect yield rates and unit cost at mass production.

  • Requesting major silhouette changes after engineering sign-off restarts the clock. Lock in the overall shape before requesting detail refinements.

Stage 3: Prototype (Physical Sample, Pre-Steel)

Timeline: 3–8 days after 3D approval

Before any steel is cut, you will hold a physical prototype of your bottle. This is a 3D-printed or rapid-tooled sample — not production material — designed purely for evaluating form, proportion, ergonomics, and label fit.

What you need to do

  • Fill the prototype with your actual formula (or a water-based proxy of the same viscosity) to check dosing feel and leak performance.

  • Test against your secondary packaging — does the bottle fit your carton depth? Does the cap clear the box lid?

  • Sign a physical approval form confirming the 3D form, proportions, and neck finish before tooling begins

white mold

What Jarsking delivers

  • One prototype unit (additional units available on request)

  • A spec confirmation document listing final agreed dimensions — this becomes the binding reference for mold machining

What to watch out for

  • The prototype material (not production resin or glass) will feel different in weight and surface texture. Evaluate shape and proportion only — not final tactile feel or clarity.

  • This is your last low-cost change window. Any structural changes requested after the prototype sign-off will require a new prototype round and will delay the steel mold start date.

  • If your team needs consumer testing at this stage, allow extra time before signing off — do not rush the approval.

Stage 4: Steel Mold Fabrication

Timeline: 35–40 days

This is the longest single stage — and the most critical. Our toolmakers CNC-machine the production mold to micron-level tolerances based on the signed-off specification.

What you need to do

  • Confirm your initial order volume before tooling begins — this determines cavity count (single-cavity vs. multi-cavity mold), which directly affects your per-unit cost at mass production.

  • Issue your tooling deposit payment. Mold fabrication does not begin until the tooling payment is received.

  • Provide vector artwork files (AI or PDF) for any surface engraving or embossing on the bottle body.

Jarsking cosmetic packaging factory interior with stacked metal molds

What Jarsking delivers

  • Progress photos at mid-point machining (approx. Day 20) and upon mold completion

  • A mold ownership certificate issued to your brand upon full payment

  • NDA-backed IP protection — your mold is held exclusively in our facility, the customer archival storage room,  and never shared with third parties

What to watch out for

  • Do not request design changes during mold machining. Any structural modification after steel cutting begins requires remachining, which adds 15–20 days and a cost surcharge.

  • If your order volume is likely to grow, discuss multi-cavity tooling upfront — it’s far more cost-effective to machine a 4-cavity mold now than to add cavities to existing steel later.

  • Keep your project manager informed of any changes to your target decoration or cap fitment during this window, as those components are being prepared in parallel.

Stage 5: Trial Production, Testing & Mass Production Sign-Off

Timeline: 5–7 days for trials + your review window

The mold produces its first real units. These trial samples are made from your actual production material — the first true representation of what your customers will hold. This stage is the final quality gate before full-scale manufacturing begins.

What you need to do

  • Receive the trial sample set (typically 30–50 units) and conduct a structured review:

    • Fill with your actual formula and check for leakage, compatibility, and dispensing performance

    • Apply your label or decoration and evaluate surface adhesion and visual alignment

    • Submit to any required drop tests, UV exposure tests, or retailer compliance checks

  • Provide written sign-off (email confirmation is sufficient) approving the trial batch for mass production.

QC

What Jarsking delivers

  • Trial sample set with full QC inspection report: dimensional measurements, surface defect AQL rating, and functional performance data

  • Any mold adjustments required based on trial feedback — minor adjustments (polish, texture, dimensional tuning) are included within the project scope

  • Production timeline confirmation: your mass production start date is locked once sign-off is received

What to watch out for

  • Allow yourself sufficient internal review time before signing off. Once mass production starts, no structural changes are possible.

  • If your formula has specific chemical compatibility requirements (e.g., high-alcohol content, active acids), ensure your fill test uses the real formula — not a placeholder.

  • Compliance documents should be reviewed at this stage. If your bottle needs to meet specific drop-test or labeling standards, flag them before sign-off, not after.

sketch for Jarsking skincare set

Why Does Custom Bottle Tooling Cost So Much?

The customer is not paying only for the visible bottle shape. Tooling cost covers the engineering and manufacturing system required to reproduce that shape reliably at production scale.

Engineers must convert a visual concept into a structure that can be filled, sealed, cooled, released, decorated, assembled, shipped, and produced consistently.

This requires decisions about:

  • Material behavior
  • Shrinkage
  • Wall distribution
  • Neck dimensions
  • Closure fit
  • Parting lines
  • Draft
  • Cooling
  • Venting
  • Surface quality
  • Machine compatibility
  • Production volume

A design error does not affect only one sample. It can repeat across every unit produced from the mold.

A mold can include much more than two bottle-shaped halves.

Depending on the process, the tooling system may need:

  • Cores and cavities
  • Blank molds and blow molds
  • Neck rings
  • Bottom plates or inserts
  • Baffles and plungers
  • Gates and runners
  • Cooling circuits
  • Venting
  • Ejector systems
  • Slides or side actions
  • Wear components
  • Alignment and mounting components

Every additional component must be designed, machined, fitted, tested, and maintained.

Production tools experience repeated cycles of heat, pressure, cooling, clamping, opening, and closing.

The appropriate mold material depends on:

  • Manufacturing process
  • Expected production quantity
  • Bottle or component material
  • Required surface finish
  • Tool complexity
  • Maintenance plan
  • Intended mold life

Longer-life tooling normally requires more demanding material preparation, machining, finishing, and validation.

Tooling cost rises when the design includes:

  • Unusual or asymmetric forms
  • Deep recesses
  • Undercuts
  • Sharp transitions
  • Integrated handles
  • Complex bases
  • Difficult neck structures
  • Heavy embossing or debossing
  • Very high-gloss surfaces
  • Tight dimensional requirements
  • Multiple moving tool components

For injection-molded components, undercuts may require moving mechanisms such as side actions. These increase the mold’s size, number of components, engineering time, and machining work.

A single-cavity tool produces one component per molding cycle. A multi-cavity tool produces several.

More cavities usually mean:

  • Higher initial tooling investment
  • More machining and components
  • More complex material-flow balancing
  • More complex cooling
  • Greater validation requirements
  • Higher output per cycle
  • Potentially lower production cost per unit

The correct cavity count should be based on forecast volume, target unit cost, machine capacity, and expected product life—not only the lowest upfront tooling price.

A mold does two jobs: it shapes the material and helps control its temperature.

Poor cooling can contribute to:

  • Long production cycles
  • Uneven shrinkage
  • Warping
  • Dimensional variation
  • Surface defects
  • Unstable production

Cooling circuits require engineering and machining, but they influence both bottle quality and long-term production efficiency.

Premium packaging often requires high-gloss, transparent, textured, engraved, or otherwise visually sensitive surfaces.

The corresponding mold may need:

  • Fine machining
  • Manual polishing
  • Texture application
  • Careful parting-line placement
  • Special inserts
  • Additional trial and adjustment work

A small defect in the mold surface can be transferred to every molded component.

Completing the mold does not finish the development process. The tool must be installed, tested, measured, adjusted, sampled, and approved.

A professional tooling program includes time for:

  • Machine setup
  • Trial materials
  • Engineering review
  • Dimensional measurement
  • Defect analysis
  • Tool correction
  • Further trials
  • Approval samples
  • Production documentation

After approval, the mold must be stored and maintained for repeat production.

Ongoing responsibilities can include:

  • Cleaning
  • Rust prevention
  • Lubrication
  • Storage
  • Inspection
  • Wear-part replacement
  • Repair records
  • Production-history records
  • Controlled access

The tooling agreement should identify which services are included and which future repairs or modifications are charged separately.

Existing Mold, Semi-Custom, or Fully Custom?

Development routeTooling investmentDevelopment timeBrand differentiationMOQ
Existing mold with custom decorationLowestShortestColor, finish, branding, closure, and secondary packaging10,000 pcs/SKU
Modified or semi-custom platformProject-dependentMediumSelected structural changes while retaining proven elementsConfirm per project
Fully custom private moldHighestLongestOriginal bottle or packaging-system structure30,000–50,000 pcs/SKU, confirmed per project

Choose an Existing Mold When:

  • Your launch schedule is the priority.
  • A proven capacity and silhouette fit the product.
  • Differentiation can come from color, finish, decoration, closure, and the box.
  • You are testing a new market or product category.
  • A proprietary structure is not central to the brand strategy.

Jarsking’s ODM route provides access to 30,000+ ready-to-use molds combined with custom CMF—color, material, and finish—and brand decoration.

Choose a Semi-Custom Platform When:

  • You need greater differentiation than decoration alone.
  • A standard neck, closure, or component system can be retained.
  • Selected changes can create sufficient visual ownership.
  • You want to control tooling investment while improving distinctiveness.

The exact scope, MOQ, and lead time must be confirmed after engineering review.

Choose a Fully Custom Mold When:

  • The bottle silhouette is a core brand asset.
  • Your package needs a proprietary structural feature.
  • Existing capacities or proportions do not meet the brief.
  • The dispensing or closure architecture is unique.
  • You are developing a long-term hero product or packaging family.
  • Your projected volume can support the tooling investment.

Jarsking’s OBM route supports project-based, design-led co-development spanning industrial design, structure, CMF, testing planning, and production industrialization.

Preguntas frecuentes

Custom tooling is a precision production system, not simply a bottle-shaped block of metal. Its cost may include structural engineering, core and cavity design, forming components, mold material, CNC machining, cooling, venting, polishing, assembly, machine trials, measurement, correction, validation, and production documentation. Complex geometry, more cavities, moving mold components, tight tolerances, and premium surfaces increase the investment.

The MOQ for packaging made from an existing Jarsking mold is 10,000 pieces per SKU. The MOQ for a fully custom mold is generally 30,000–50,000 pieces per SKU, with the final requirement confirmed according to the project, material, tool structure, decoration, and production plan.

Tooling is generally an upfront development investment, but the quotation should define exactly what it includes. Later structural modifications, replacement inserts, major repairs, wear components, transfers, or new cavities may create additional costs. Storage and maintenance terms should also be confirmed in the tooling agreement.

A prototype is mainly used to evaluate shape, proportions, ergonomics, visual appearance, label area, and basic component arrangement before production tooling. A production-molded sample is made with the actual tool and intended production material. Leakage, compatibility, final surface quality, shrinkage, dimensional performance, and mass-production suitability should be evaluated using appropriate production samples and testing.

Not always. Some projects can use a compatible existing preform and require only a new bottle blow mold. Other projects need a custom preform because of the bottle’s neck, weight, proportions, wall distribution, or performance requirements. Jarsking determines the appropriate tooling scope during the feasibility review.

Mold ownership, exclusivity, storage, permitted use, maintenance, repair, modification, and transfer rights should be defined in the project quotation and tooling agreement. Do not assume that every supplier uses the same policy. Ask for these terms in writing before authorizing the tooling payment.

Solicitud de presupuesto